

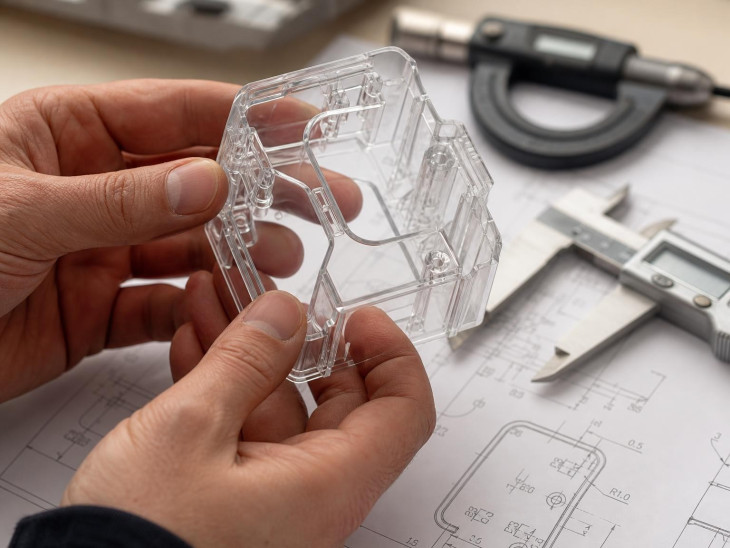
Injection molding remains one of the most widely used methods for producing consistent, repeatable plastic components, from electronic housings and automotive brackets to medical devices and everyday consumer goods. Yet producing a reliable molded part takes far more than picking a plastic and sketching out a shape. Geometry, tolerances, mold design, cooling behavior, and the part's intended use all have to work together as a system. This article centers on one core idea: designing for manufacturability early can help prevent defects, rework, delays, and unnecessary tooling expense.
Why Design for Manufacturability Matters
Design for manufacturability (DFM) means shaping a part so it can be produced efficiently and consistently using the chosen process. Even a seemingly simple design can run into trouble with plastic flow, cooling and shrinkage, part ejection, mold complexity, dimensional repeatability, and assembly fit. Changes made on a digital model before tooling begins are almost always easier and cheaper than modifications to a finished steel mold. That said, manufacturability has to be balanced against functional, aesthetic, regulatory, and performance requirements—DFM is a constraint to design within, not a substitute for sound engineering judgment. General guidelines should always be checked against resin datasheets and, where warranted, mold-flow simulation. When researching production options, readers may find it useful to review technical information from resources such as Texas Injection Molding, while still applying independent design principles to judge whether a given part is actually suited to the process.
Select the Material Before Finalizing the Geometry
Material selection should happen early, since resin behavior drives many geometry decisions. Key characteristics to weigh include strength and stiffness, impact resistance, temperature capability, chemical resistance, flexibility, UV and environmental resistance, shrinkage behavior, and any regulatory or food-contact requirements. Amorphous plastics tend to shrink less—and more predictably—than semi-crystalline plastics, which can shrink more and sometimes unevenly depending on flow direction. Choosing a resin based purely on price or ease of processing can create downstream problems with strength or dimensional stability. Always confirm properties using the current technical datasheet for the specific grade, including any fillers or reinforcements.
Key takeaway: The material, part geometry, and mold design should be evaluated as one system, since changing one will almost certainly affect the others.
Maintain Practical Wall Thickness
Uniform wall thickness supports even filling and cooling. Thick or uneven sections commonly lead to sink marks, internal voids, warping, longer cooling cycles, and residual stress. Coring out solid mass, and using ribs and gussets instead of thick walls, helps maintain strength while keeping thickness consistent. Abrupt thickness transitions should be smoothed into gradual ones wherever possible. Exact thickness targets vary by resin, part size, and flow length, so resin-specific guidance should always take priority over a single universal number.
Illustrative example: Consider a plastic enclosure that develops visible depressions around thick screw bosses after molding. A design review might reveal that the bosses were modeled as solid cylinders rather than cored features. Converting them to cored bosses with properly proportioned wall thickness and supporting ribs can reduce the mass driving the sink marks, improving surface appearance without weakening the mounting points.
Add Draft, Fillets, Ribs, and Bosses Early
Draft angle is a slight taper applied to surfaces running parallel to the mold-opening direction. Adequate draft lets a part release cleanly, cutting down on drag marks, deformation, and excessive ejection force. Textured surfaces typically need more draft than smooth ones, and the exact amount depends on texture depth, resin, mold finish, and part geometry.
Rounded internal corners, or fillets, improve plastic flow, reduce stress concentration, lower the risk of cracking, and simplify mold machining. Sharp internal corners should generally be avoided unless there's a functional reason to keep them.
Ribs add stiffness using less material than a solid thick wall would, but poorly proportioned ribs can cause sink marks, while bosses that are too thick relative to the adjoining wall can crack or distort. Ribs and bosses should be sized according to the selected material and wall thickness, ideally validated through engineering review or simulation.
Plan Gates, Parting Lines, and Undercuts
Gates control where molten plastic enters the cavity, runners deliver material to the gate, and the parting line marks where the mold halves meet. Gate location shapes the fill pattern, weld-line formation, air entrapment, surface appearance, packing pressure, and dimensional consistency, so it needs to be chosen with both function and appearance in mind. Parting-line placement, in turn, affects flash, visible seams, tooling complexity, and ejection. Undercuts—features that would otherwise trap the part in the mold—often call for slides, lifters, inserts, or a change in geometry.
A short checklist can help during early design review:
- Can the part release from the mold without interference?
- Are undercuts truly necessary?
- Is the parting-line location acceptable on the finished product?
- Can the gate be positioned without compromising function or appearance?
- Are ejection areas strong enough to avoid distortion?
Set Realistic Tolerances
A tolerance describes the acceptable variation from a nominal dimension. Molded dimensions can shift due to resin shrinkage, cooling conditions, mold wear, part geometry, moisture content, process variation, and even the measurement method used. Tight tolerances should be reserved for dimensions that affect fit, sealing, movement, safety, or performance, since unnecessarily tight specs drive up tooling, inspection, and production costs. Identifying critical-to-function dimensions separately from purely cosmetic ones, and running a tolerance stack-up across an assembly rather than judging each dimension in isolation, leads to far more realistic specifications. No single tolerance value is universally achievable—final specs should be worked out jointly by the designer, mold builder, processor, and quality team.
Anticipate and Prevent Common Defects
Several recurring defects trace directly back to design choices: warping often stems from uneven cooling or inconsistent thickness; sink marks commonly trace to thick sections, bosses, or ribs; voids may form from internal shrinkage in thick areas; flash can signal parting-surface or pressure issues; short shots may result from restricted flow or inadequate venting; and weld lines form where separated flow fronts rejoin, sometimes affecting strength or appearance. Because defects often have more than one contributing cause, design changes should be backed by process data rather than a single assumption.
Illustrative example: A warped flat panel might initially get blamed on machine settings, but mapping wall thickness, reviewing gate placement, and analyzing cooling channel layout often reveals a combination of contributing factors rather than one isolated cause.
Validate the Design Before Tooling
A staged validation approach cuts down on risk before any steel gets cut: review the 3D model and drawings, confirm material and performance requirements, check draft and wall thickness, review parting lines and ejection, run mold-flow analysis when it's justified, build prototypes, and measure critical features using an agreed inspection method. Prototypes often surface assembly or ergonomic issues that simulation alone can't predict. Documenting assumptions, approved materials, critical dimensions, and change history supports traceability, which matters even more in regulated applications that require additional testing and quality controls.
Final Design Review Checklist
- Material properties and environmental requirements are documented.
- Wall thickness is reasonably consistent.
- Thick sections are cored where practical.
- Draft is included on mold-opening surfaces.
- Ribs, bosses, and transitions are proportioned appropriately.
- Corners include suitable radii.
- Gates, vents, parting lines, and ejection points have been considered.
- Critical tolerances are tied to function.
- Likely defects have been assessed.
- The design has undergone appropriate technical review before tooling.
When to seek specialist review: Regulated products, tight-tolerance assemblies, high-temperature applications, and parts with complex undercuts generally benefit from additional engineering or tooling expertise before a design is finalized.
Build Reliability Into the Design
Reliable molded parts come from coordinated decisions about material, geometry, tooling, processing, and inspection—not from any single choice made in isolation. The best design isn't necessarily the simplest or the thickest one; it's the one that meets functional requirements while still supporting consistent filling, cooling, release, and measurement. Bringing in experienced design, materials, tooling, and quality professionals early pays off especially well for complex or high-consequence applications. A structured DFM review before mold construction can protect both product performance and project resources.